Challenge: Grinding cermet round bars with centerless grinding wheels
Cermet boasts superior hot hardness, yet this property also makes it much harder to grind.
This paper presents performance tests on our company’s centerless grinding wheels developed for machining cermet round bars. The test details are as follows:
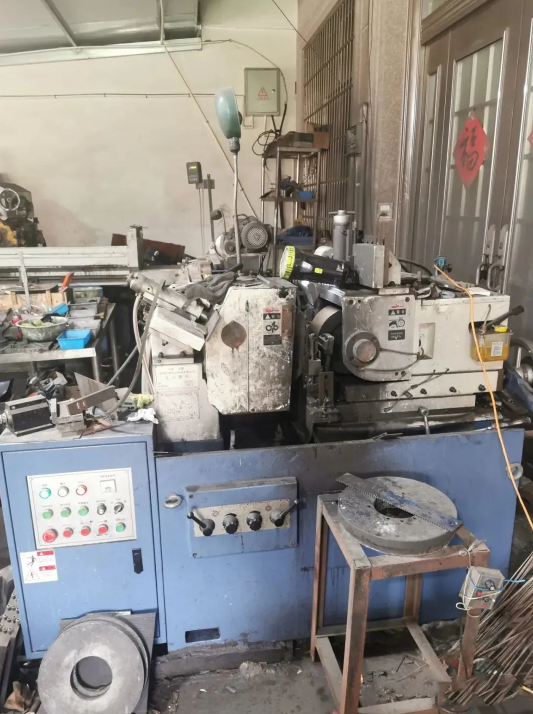
Test equipment: 1040 centerless grinder manufactured by Wuhu Zhongchi
Grinding Wheel specification: 1A1 350×127×10×125, 120#, special for cermet
Workpiece specification: φ10×100 mm
Workpiece material: DTN680
Machining parameters: Stock removal of 0.06 mm per pass;
Traverse speed 250 mm/min
Machining accuracy: End-to-end runout of ground bars ≤0.001 mm
This type of centerless grinding wheel is also suitable for cemented carbide.
Relevant machining parameters:
Workpiece specification: Cemented carbide bar φ20×180 mm
Grinding parameters: Stock removal of 0.08 mm per pass;
Traverse speed 250 mm/min
Machining accuracy: End-to-end runout of ground bars ≤1 μm
Compared with the grinding wheels previously used by the customer, the test results show a 50%~200% efficiency improvement, and the product has gained customer recognition.