At present, hot-pressed white corundum wheels are mostly adopted in tap grinding, which are dressed with diamond forming rollers to form the required shape. CBN wheels are different from ordinary abrasive wheels, with different operating and dressing parameters. Our company has carried out a large number of experiments and obtained the dressing parameters for CBN wheels.
Wheel dressing is to make the geometric dimension and precision of the wheel meet requirements macroscopically, and fracture the abrasive grains of the wheel to form sharp cutting edges. Generally, there are two ways for wheel dressing on tap grinders: roller path forming and direct forming with forming rollers.
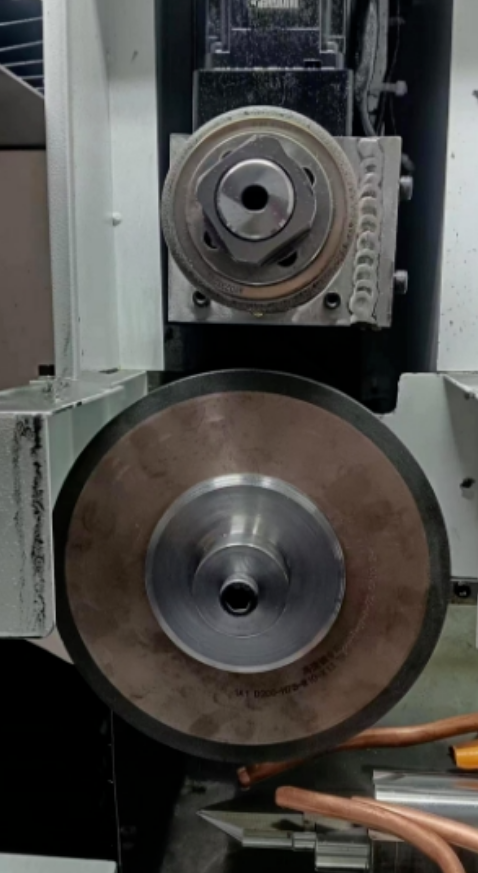
Dressing parameters for roller path forming:
Machine: Xiaotian CNC fluting machine Roller size: 14F1 90×32×R4×16T, sintered forming CBN wheel size: 1A1 200×32×10×13, B107 Purpose: Dress the CBN wheel into the shape required for standard φ24 tap flutes
Dressing parameters: Dressing roller speed: 1800 rpm; CBN wheel speed: 1000 rpm; single dressing depth: 0.035 mm; dressing speed setting value: 200. Approximately 13 seconds per stroke.
Dressing efficiency: 250 dressing passes are required to dress from the original 1A1 profile to the required shape, taking about 55 minutes. Pre-forming a certain profile during CBN wheel production can effectively reduce dressing time and roller loss.
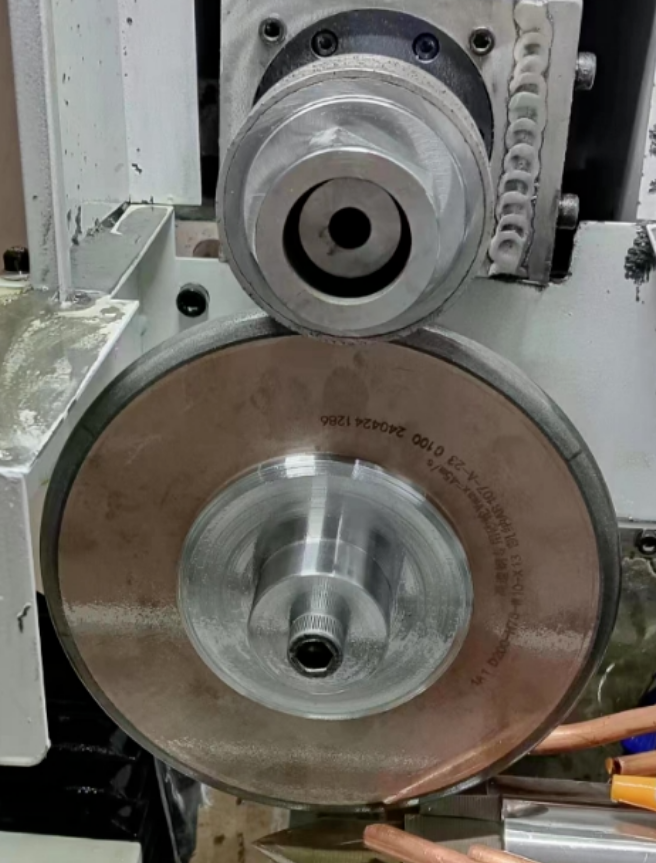
Dressing method with forming roller:
Machine: Xiaotian CNC fluting machine Roller size: 4XM24 standard forming roller, electroformed CBN wheel size: 1A1 200×32×10×13, B107 Purpose: Dress the CBN wheel into the shape required for standard φ24 tap flutes
Dressing parameters: The CBN wheel is firstly rough dressed by the wheel manufacturer on a dressing machine. After installed on the machine, it is dressed with the forming roller. Dressing roller speed: 1800 rpm; CBN wheel speed: 1000 rpm. Align the forming roller with the CBN wheel and feed manually. After the forming roller contacts the CBN wheel, feed 0.01 mm and carry out mutual grinding for 30~60 seconds. Judge the infeed amount and grinding time by sound, then repeat this process until the roller surface fully contacts the CBN wheel surface.
Dressing efficiency: It takes about 30~60 minutes to fully dress the CBN wheel. Pre-forming a certain profile can effectively reduce dressing time and roller loss.