With the widespread use of wood lock hole machines, the demand for carbide woodworking lock hole cutters keeps rising.
During production of such cutters, long slots need to be ground. The slotting wheel must remain sharp throughout the grinding process; otherwise, cutter breakage may easily occur.
Besides, high market volume requires automated production. The dressing interval of the slotting wheel, namely how long the wheel retains sharpness, should be as long as possible to reduce operators’ workload.
Moreover, retention of the wheel radius directly affects dimensional stability of the cutters, which poses high challenges for wheel manufacturers.
In response to customer requirements, our company has optimized the formulation and manufacturing process of high-power slotting wheels through multiple trials,
and developed this slotting wheel tailored for such working conditions. Test details are as follows:
**Test Equipment:** DJ S500T+ (Spindle Power: 6kW)
**Test Grinding Wheel:** 1A1 125×31.75×10×12, D64-M76
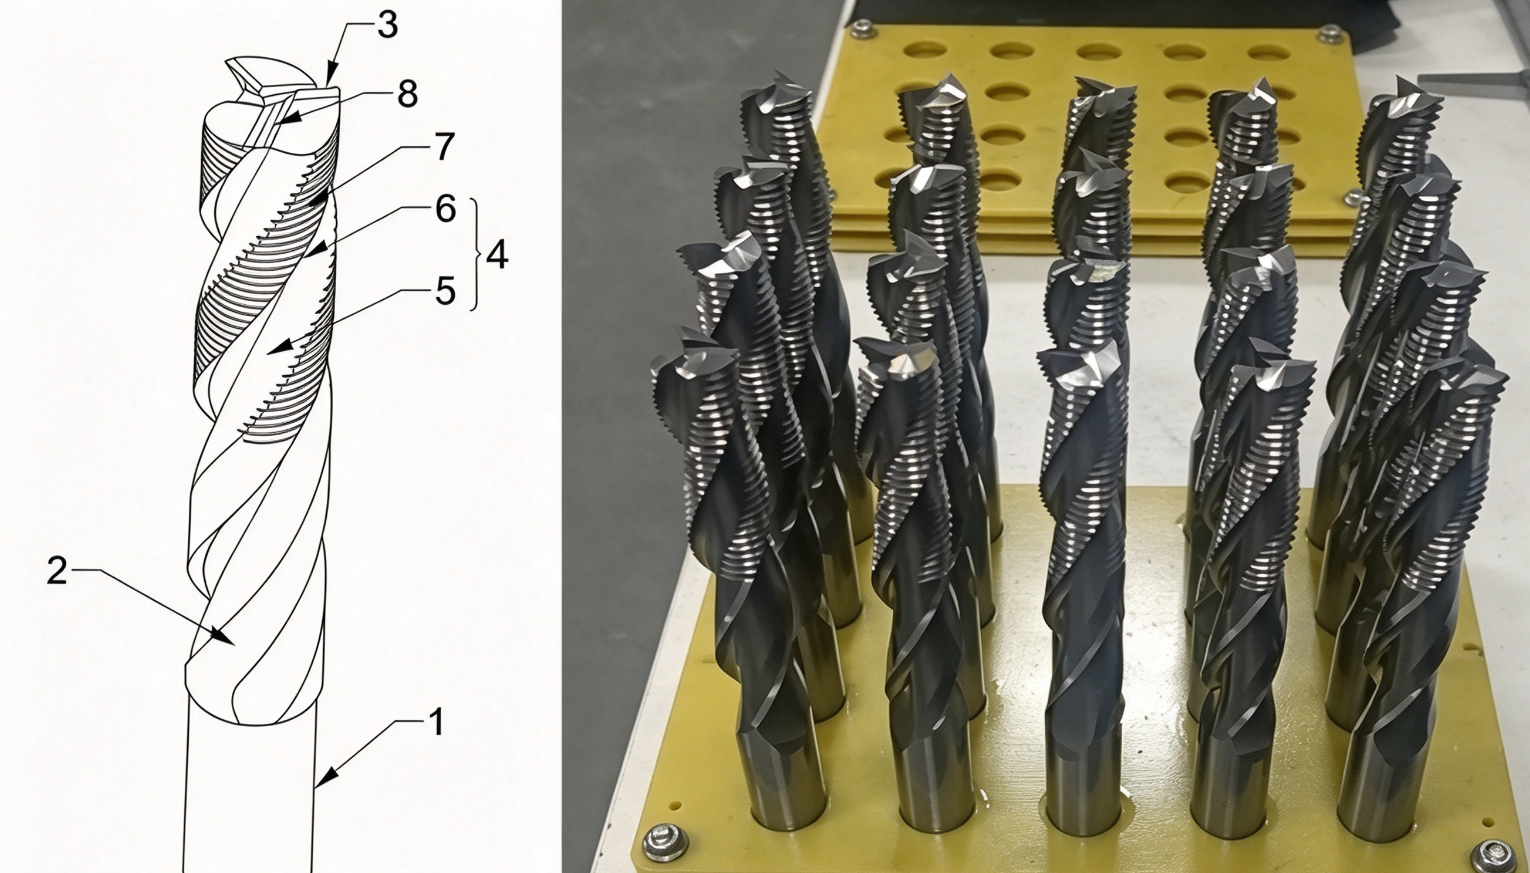
**Test Cutter:** 16mm diameter, 3-flute end mill, cutting length 105mm, helix angle 24°
**Grinding Parameters:** Wheel peripheral speed: 18 m/s; 1st pass depth of cut: 1.75 mm, feed rate 160; 2nd pass depth of cut: 2 mm, feed rate 180
The test results for tools made of virgin material are as follows:
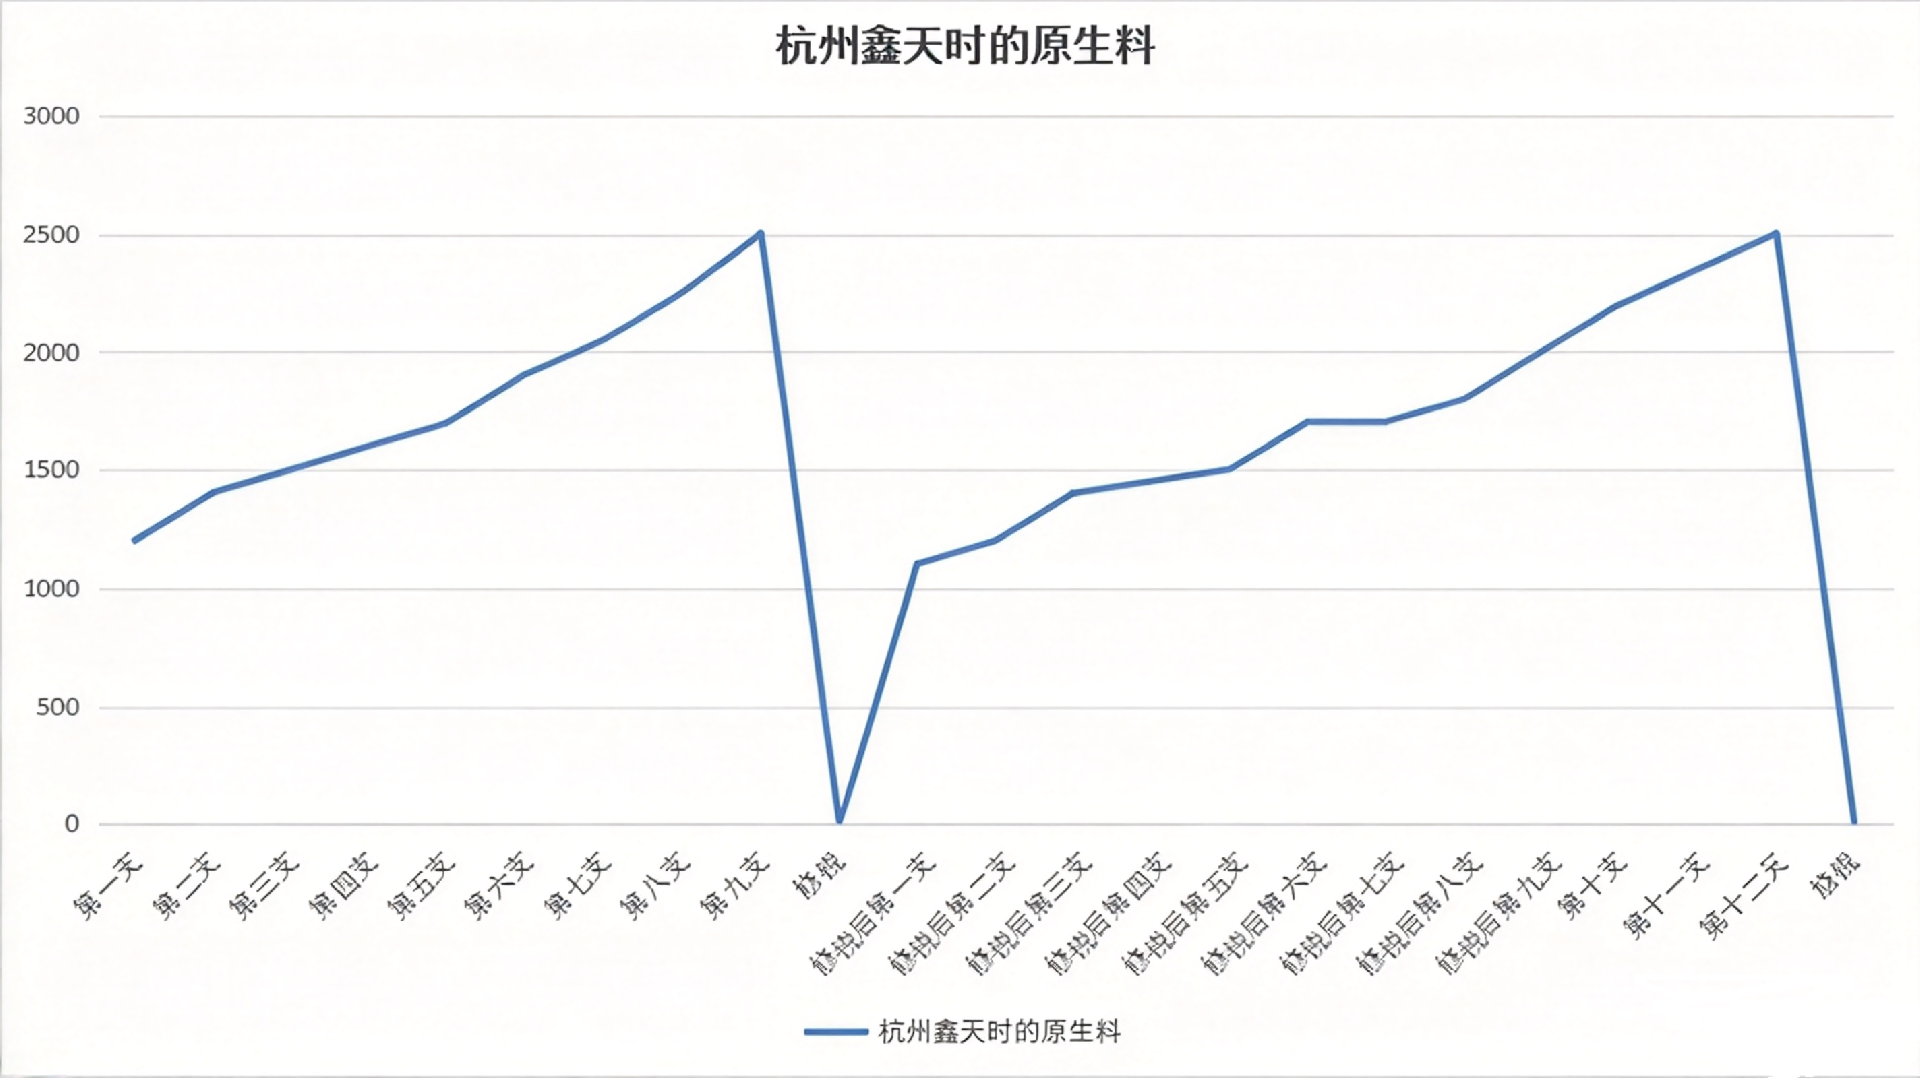
The wheel can machine cutters directly after dressing without extra sharpening. Sharpening is required when grinding power reaches 2500W.
The wheel needed sharpening after the 9th cutter. After sharpening, it machined another 12 cutters before re-sharpening. The average sharpening interval is around 12 pieces.
Machining time per cutter: approx. 45 mins. Sharpening cycle: approx. every 10 hours.
Wheel wear: After machining 21 cutters, wheel diameter loss 0.09 mm; radius remains roughly unchanged at ~0.2 mm.
Test Results – Recycled Material Cutters
The wheel can machine cutters directly after dressing without extra sharpening. Sharpening is required when grinding power reaches 2500W.
The wheel needed sharpening after the 7th cutter. After sharpening, it machined another 7 cutters before re-sharpening. The average sharpening interval is around 7 pieces.
Machining time per cutter: approx. 45 mins. Sharpening cycle: approx. every 5.5 hours.
Wheel wear: After machining 14 cutters, wheel diameter loss 0.06 mm; radius remains roughly unchanged at ~0.2 mm.
**Summary:** Recycled material is harder to grind than virgin material. This wheel delivers stable sharpness and profile retention. Further application scenarios are subject to customer verification.