In actual saw blade production, the selection of grinding wheel grit size directly affects the quality of saw teeth edges, which further determines the cutting performance of saw blades.
Therefore, proper grit selection is critical. The following explains grit selection with magnified photos of saw teeth.
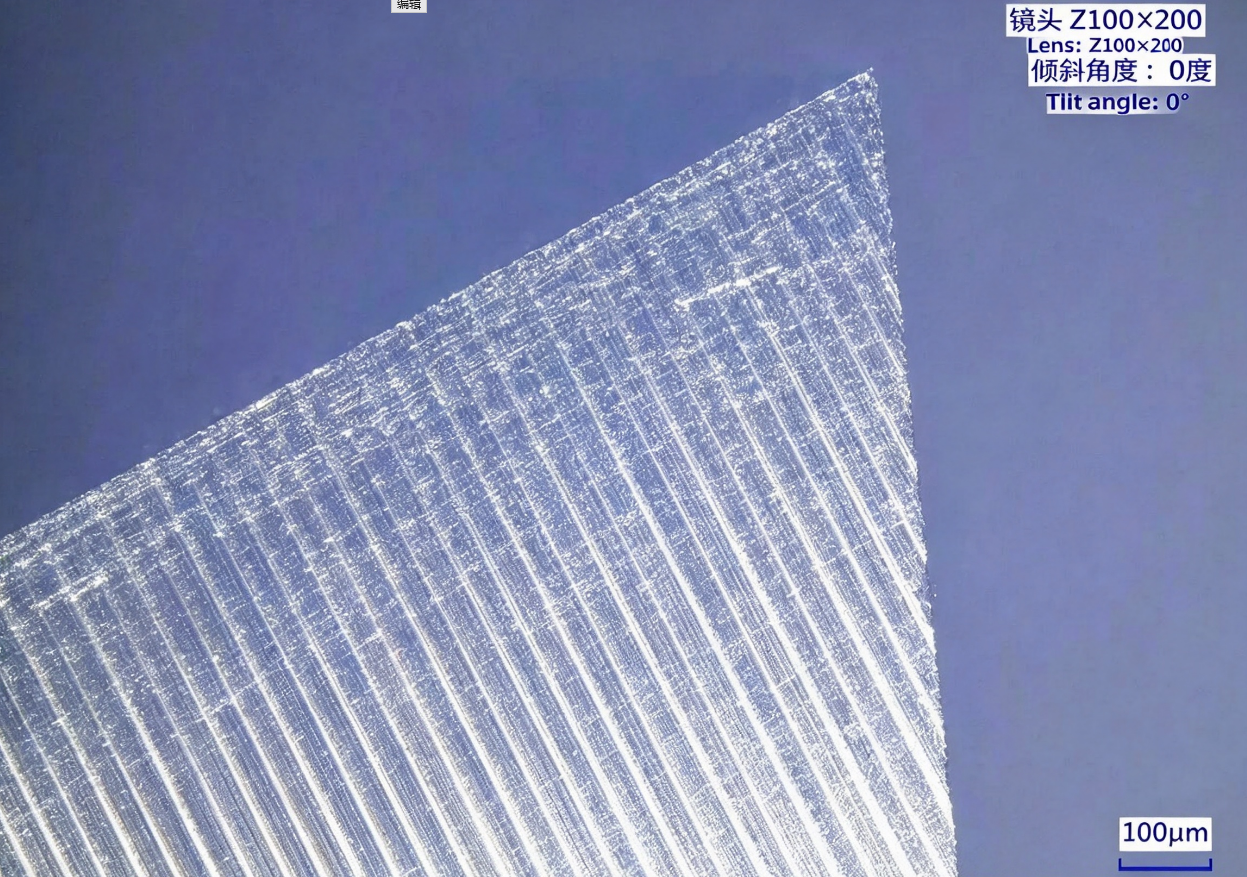
The magnified photo of a perfect saw tooth is shown below, finished by a 280/600 grit grinding wheel:
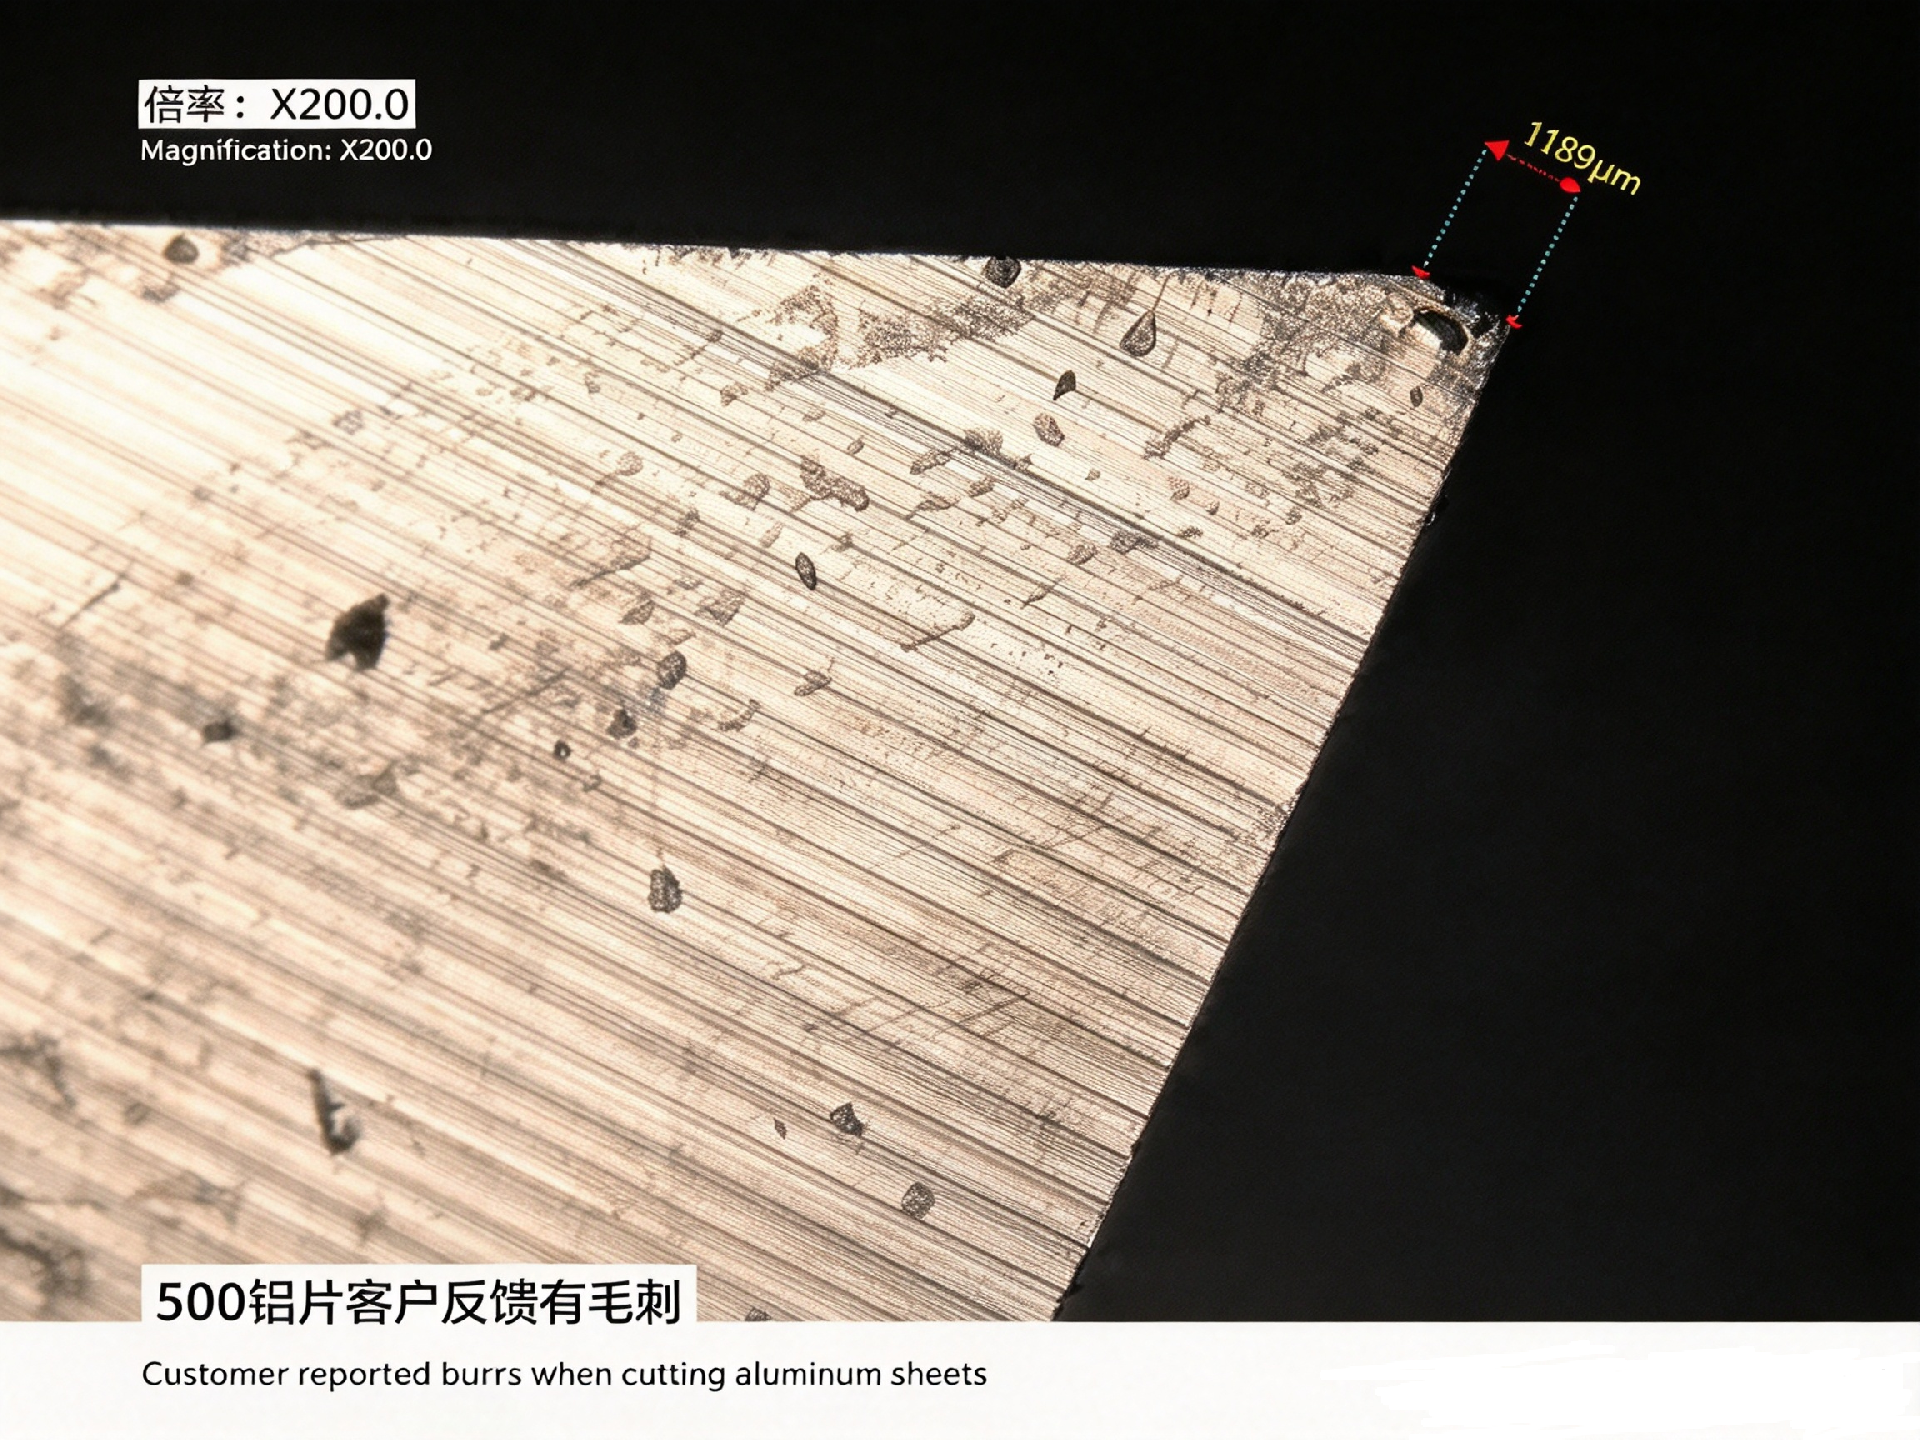
During service, saw blades become dull once tooth tips wear to a certain extent and require resharpening. Below is the magnified photo of saw teeth on an aluminum-cutting saw blade awaiting resharpening:
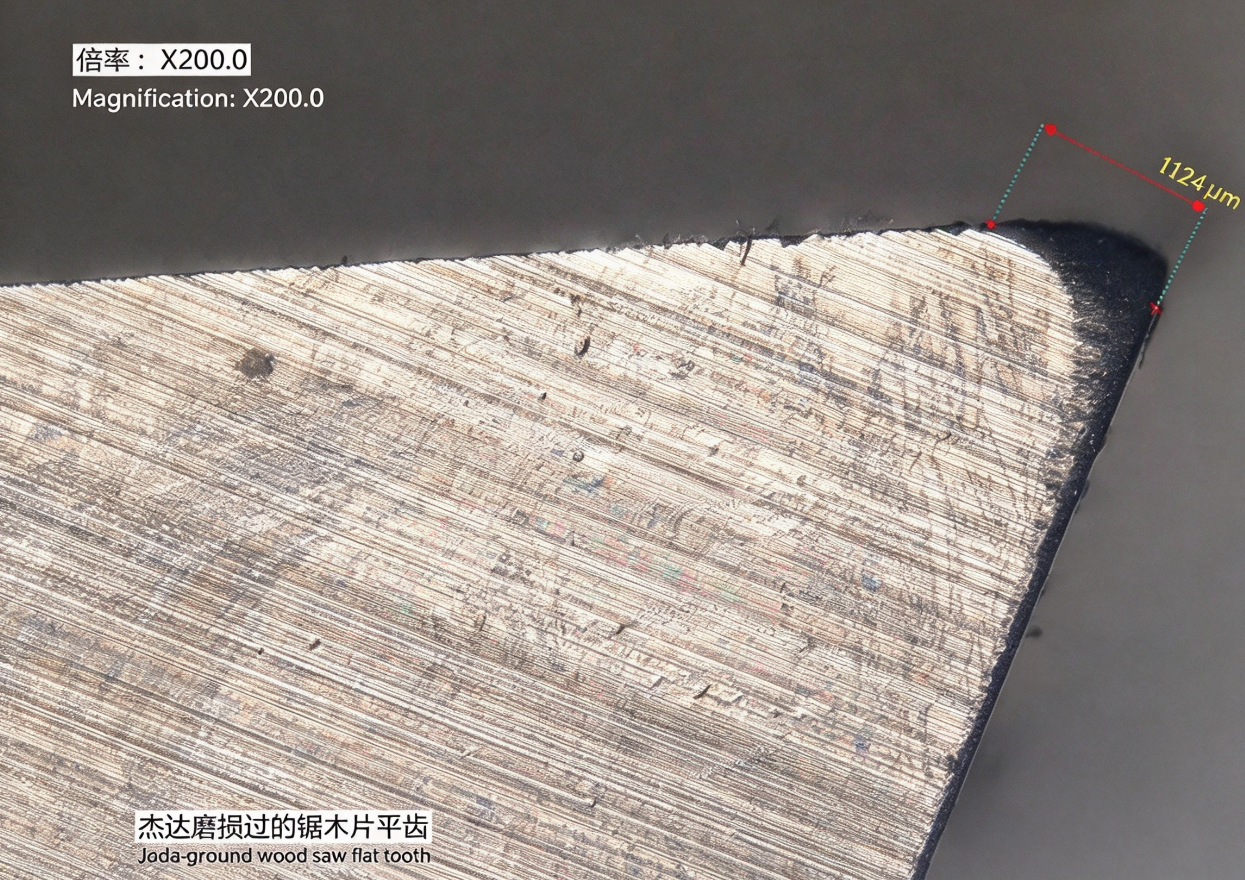
Below is the magnified photo of saw teeth on a wood-cutting saw blade awaiting resharpening:
By observing the wear width at tooth tips from the two photos: When the tooth tip wear of an aluminum-cutting saw blade reaches 0.089 mm, customers report burrs on aluminum profiles and resharpening is needed.
For wood-cutting saw blades, resharpening is required when tooth tip wear reaches 0.247 mm as the blade turns dull.
Hence, the initial integrity of cutting edges is vital to saw blade service life. Edge integrity depends on tip material, machine condition and grinding wheel grit size.
Shown below are magnified photos of saw teeth ground with 240# and 400# grinding wheels for clearance faces:
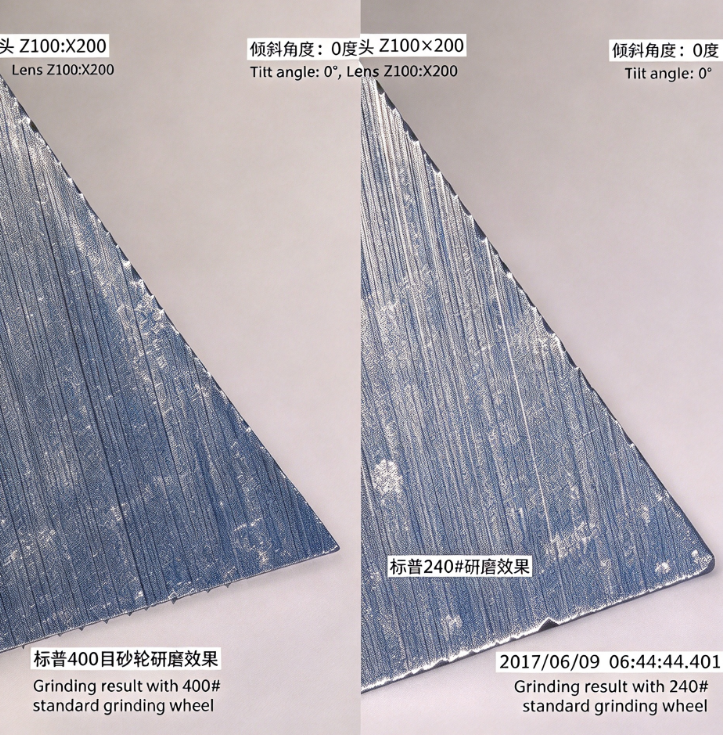
The photos clearly show that the 400# wheel produces much better saw tooth integrity than the 240# wheel.
We also need to consider the grinding wheel rotation direction for edge integrity. Below are magnified photos of rake faces sharpened by grinding wheels of different grit sizes:
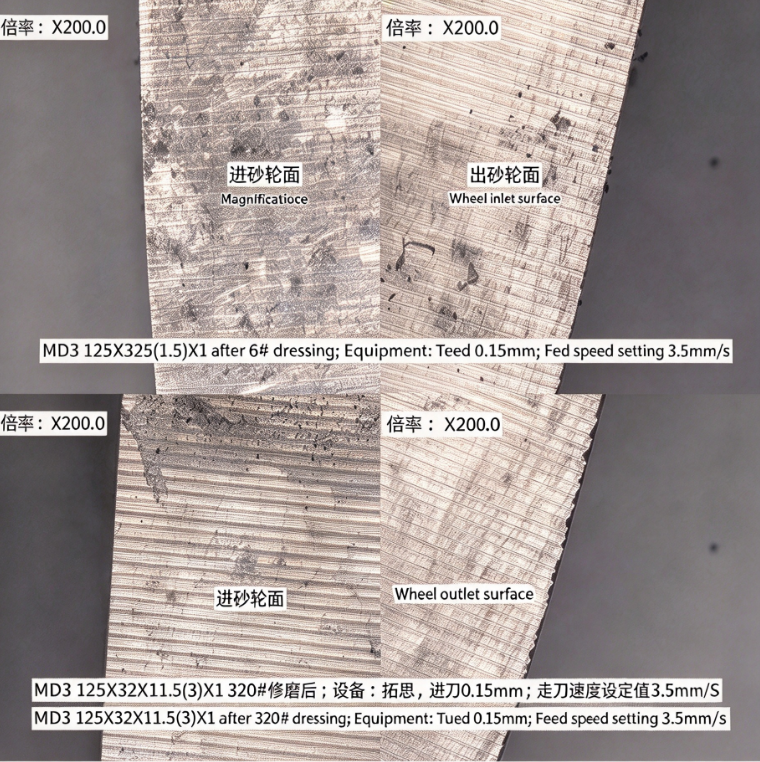
The photos indicate that both 600# and 320# rake-face wheels maintain intact edges on the wheel entry side.
However, on the wheel exit side, the 600# wheel achieves far superior edge integrity compared with the 320# wheel.
In summary: Wood-cutting saw blades have relatively lower requirements. For cost efficiency, a coarser option is acceptable: use 180/400 double-layer wheel for clearance faces and 320# wheel for rake faces.
Aluminum-cutting saw blades require 280/600 double-layer wheel for clearance faces and 600# wheel for rake faces. This ensures excellent saw tooth integrity and sharp cutting performance.